Excessively Fast Drying Rate in Coating Machines: Common Defects & Troubleshooting发表时间:2026-05-28 12:36 What problems will an excessively fast drying rate of a coating machine cause? After working in the coating industry for years, we often encounter perplexing issues: even when the oven temperature remains unchanged, unexpected defects suddenly appear on finished products. Or when launching new products, no matter how you adjust the parameters, the problems persist. In such cases, seasoned veterans will usually ask one question: Have you tested the drying curve? More often than not, people have no answer.
In fact, most issues stem not from the coating head, but from the oven — especially an overly fast drying rate. I once debugged a slot-die coating line for optical protective films, using a solvent-based acrylic coating with a wet film thickness of merely 15 micrometers. The trial production ran smoothly at first, but when the line speed was increased to 25 meters per minute, fine orange-peel-like textures emerged on the coated surface. Under reflected light, countless tiny granular blemishes covered the entire film. Initially, we assumed the coating head was faulty. We recalibrated the gap of the comma doctor blade, inspected the feed pump flow rate, and replaced filter cartridges twice. After a full day of troubleshooting, the defect still existed. Then an experienced senior technician took a quick look and suggested: Lower the temperature of the first oven zone by 10 degrees Celsius. Skeptical, I followed the advice — and the strange texture disappeared instantly. It was such a simple fix, yet it made me realize how easily we overlook drying conditions.
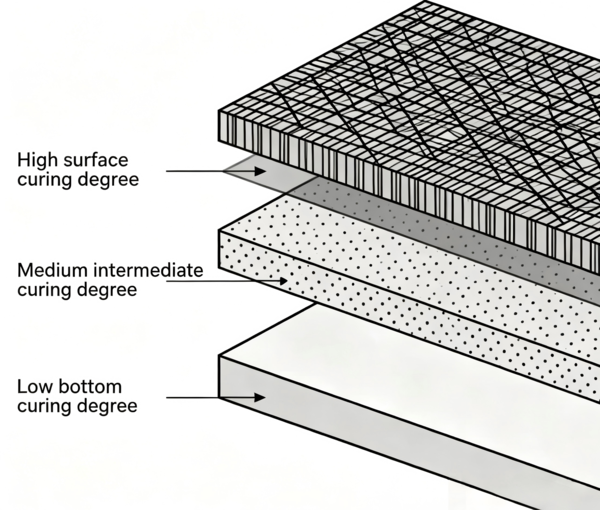
The root cause was excessive drying speed: the coating surface dried and solidified prematurely, while solvent trapped inside continued to evaporate. The expanding internal solvent bulged the surface, forming the orange-peel effect. Below is a detailed breakdown of all potential problems triggered by out-of-control drying rates, from the moment the wet coating enters the oven to final rewinding.
1. Coating Surface DefectsPremature surface drying is the most typical issue. Rapid evaporation of surface solvent forms a dense solid film, locking residual solvent inside the coating. This leads to a series of flaws including bubbles, pinholes, orange peel and craters. In severe cases, the coating will crack extensively, rendering the product unusable.
2. Poor AdhesionThe coating may appear dry, yet fail to bond firmly to the substrate. Many operators notice the coating peels off easily upon contact or fails cross-hatch adhesion tests, and immediately blame inadequate primer treatment. This is not always the case. Excessively fast drying causes uneven migration of resin and additives within the coating. Adhesive components near the substrate become immobilized before they can fully bond, resulting in poor adhesion.
3. Uncontrollable Surface GlossThis is a critical concern for high-gloss coating applications. Insufficient leveling time due to rapid drying increases surface roughness and drastically reduces gloss. Conversely, overly slow drying will cause haze or blushing. Striking the right balance for drying speed is always challenging.
4. Substrate DeformationHigh oven temperature or excessive air volume heats the substrate, causing stretching, shrinkage and wrinkling. After rewinding and cooling, the release of internal shrinkage stress leads to product warpage, which severely hinders subsequent processes such as die-cutting and lamination.
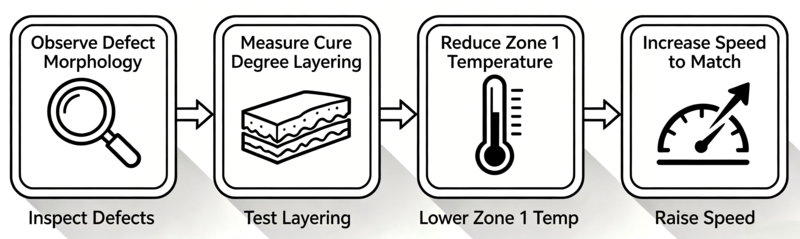
5. Static Electricity & Safety HazardsFast drying is usually accompanied by high temperatures and strong airflow. For non-conductive film substrates, static electricity builds up rapidly. Static charge attracts dust and creates surface blemishes; in extreme cases, it may even generate sparks. Given the flammable nature of solvent-based coatings, this poses major fire and explosion risks. Solutions for Excessively Fast DryingWhen you suspect drying speed is the culprit, do not rush to adjust the coating head. Follow these steps instead:
1. Identify defects by appearance Orange peel, pinholes, bubbles and cracks mostly result from premature surface drying. Hazy surfaces and low gloss indicate insufficient leveling time. Wavy patterns or longitudinal stripes are usually caused by unstable tension or direct airflow from air nozzles inside the oven.
2. Test layered curing degree Collect samples right after they exit the oven, and test the curing degree of both the surface and the bottom layer. A large gap between surface and bottom curing levels confirms premature surface drying.
3. Adjust oven zones section by section Gradually lower the temperature of each oven zone and adjust air volume accordingly. Prioritize the first zone, where solvent evaporates most intensely. If defects improve after adjustment, you are on the right track.
4. Match line speed appropriately Slow line speed also leads to over-drying, as the coating stays in the oven for too long. Try increasing the line speed while moderately raising oven temperature to balance the drying rate. This "fast line speed + matched drying" principle is widely applied on high-speed coating lines. |