Why does PET film stick to rubber rollers after corona treatment?Issuing time:2026-05-28 10:40 After PET film undergoes corona treatment and passes through the coating head, it fails to run steadily along the production line and instead sticks to the rubber rollers and winds up. This issue can lead to unplanned downtime for cleaning in mild cases, or even complete scrapping of entire film rolls in severe situations. What is most frustrating is that the previous roll ran perfectly normally, while the next one suddenly develops sticking problems.
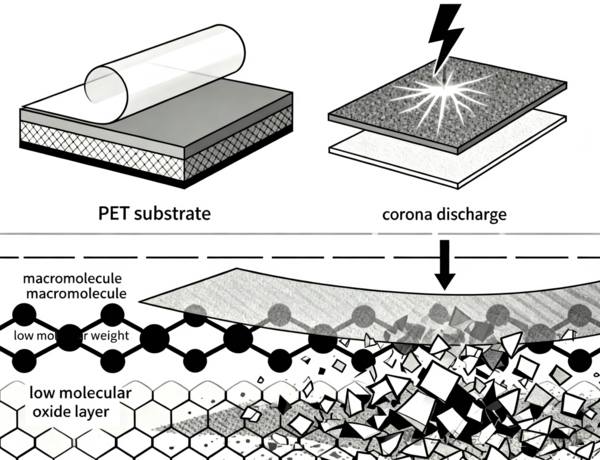
I. Changes of PET Film after Corona TreatmentBasic Properties of PET FilmPET is a non-polar material with an initial surface energy of approximately 38 mN/m, resulting in poor adhesion to adhesives and inks. The core principle of corona treatment is to break down air via high-frequency and high-voltage electricity in an open capacitive system, generating plasma to bombard the PET film surface. This process introduces polar functional groups such as hydroxyl groups and carboxyl groups onto the film surface, raising the surface energy to 48–56 mN/m or even higher.
However, these newly formed polar groups are unstable. They gradually migrate and rearrange toward the interior of the PET substrate, causing a continuous drop in surface energy — a phenomenon known as surface energy attenuation. While excessive attenuation may lead to poor printing adhesion, the primary cause of roller sticking is another byproduct of corona treatment: low molecular weight oxidized material (LMWOM). Intense energy from corona discharge fractures the macromolecular chains on the PET surface, forming loose, low-molecular-weight oxidized fragments. These fragments are similar to fine powder attached to the film surface with extremely low mechanical strength. Under combined pressure and heat when passing over rubber rollers, the fragments easily peel off and adhere to roller surfaces. As accumulation continues, the film is eventually pulled up by the rollers. This problem originates from the PET film itself rather than the coating adhesive. Seasoned industry practitioners have also found that over-intense corona treatment backfires. Films with excessively high corona values sometimes deliver inferior bonding strength compared to those with moderate corona treatment. Excessive corona produces an overly thick weak boundary layer (LMWOM). In this case, adhesives bond only to the loose fragmented layer instead of the PET substrate, so delamination occurs easily under external force.
II. Troubleshooting GuidelinesBefore adjusting machine parameters, observe the sticking condition on-site to pinpoint the root cause.
2.1 Identify the Stuck RollerDifferent rollers indicate distinct issues: ·Coating rubber roller: The problem generally lies with the adhesive or poor surface finish of the roller. ·Back roller: Defects on the back side of the substrate, such as unintended corona treatment on the reverse side or surface contamination. ·Guide roller / Pass roller: Changes in the surface condition of the substrate during operation or static electricity buildup.
2.2 Adhesion Morphology·Full-surface sticking: Severe corona attenuation or massive LMWOM precipitation, resulting in excessive affinity between the film and roller surface. ·Regular partial sticking: Out-of-round rollers or uneven corona treatment leading to inconsistent lateral surface energy. ·Edge-initiated spreading sticking: Improper corona treatment width and corona discharge overflow at the film edges.
2.3 Key Confirmation Questions1. Is this a sudden failure or a recurring long-term issue on the machine? 2. Did the problem emerge after switching to a new batch of PET film, or occur randomly within the same batch? 3. Does sticking happen occasionally or to every roll? Answers to these questions can greatly narrow down the troubleshooting scope. III. Film Surface IssuesOver 90% of PET roller sticking problems stem from abnormal film surface conditions. 3.1 Dyne Level TestA single dyne pen test (e.g., 38 mN/m) cannot reflect real conditions. It is recommended to use a complete set of dyne pens (38, 40, 42, 44, 46, 48 mN/m) to test the left, middle and right positions across the film width. Draw a 100 mm-long line on the film surface and check if the liquid beads up within 2 seconds. A qualified dyne level does not rule out LMWOM issues. 3.2 Weak Boundary Layer (LMWOM) InspectionDyne pens only measure surface tension and cannot detect the poor tensile strength of LMWOM. Two practical testing methods: 1. Apply a piece of clean adhesive tape firmly to the corona-treated film surface, then peel it off quickly. Visible white powder residue on the tape indicates severe LMWOM. 2. Rub the corona-treated surface firmly with a clean finger. White residue on the finger confirms the presence of a weak boundary layer.
Solutions for LMWOM: Reduce corona power to the minimum required to reach the target dyne level; or arrange coating immediately after inline corona treatment to shorten the retention time of LMWOM on the film surface. 3.3 Corona Treatment TimelinessThe dyne level of corona-treated PET will inevitably attenuate over time, accelerated significantly by high temperature and high humidity. For purchased pre-corona-treated PET film, severe attenuation may occur after storage for more than 24 hours. PET film containing slip agents attenuates even faster, with dyne levels dropping below the usable standard within 24 hours.
Handling Measures: Require suppliers to mark the corona treatment date on pre-treated film. Test the dyne level before production. Return severely attenuated film or perform supplementary inline corona treatment. 3.4 Accidental Corona on Film Reverse SideAir ingress between PET film and the corona roller or uneven pressure from the front rubber pressure roller will cause discharge to spread to the film back side. Once the reverse side gains higher surface energy from unintended corona treatment, it will stick to back rollers easily. Verification & Solutions: Test the dyne level of the film’s non-corona side; an abnormally high reading confirms this issue. Adjust pressure balance of the front pressure roller, control the radial runout of the corona roller within 0.05 mm, and install baffles on both sides of the corona roller to limit discharge range. IV. Rubber Rollers & EquipmentIf no film surface defects are found or sticking persists after film treatment, inspect rollers and equipment. 4.1 Roller Surface ConditionA worn rubber roller with increased surface micropores has a larger contact area with the film, raising friction and accelerating LMWOM accumulation. After long-term operation, plasticizers and low-molecular substances inside rubber rollers migrate to the surface and form sticky deposits, especially in high-temperature workshops.
Inspection Checklist: ·Visible scratches or abrasion on roller surfaces ·Embedded hardened adhesive or foreign particles ·Latest cleaning time and cleaning agent used ·Service life and Shore hardness of the roller
Cleaning Suggestion: Use suitable solvents to clean roller surfaces, then wipe with clean lint-free cloths. Replace rollers promptly if surfaces are hardened or cracked — the cost of a new roller is far lower than losses from mass scrapped products. 4.2 Roller Cover MaterialConventional rubber rollers are prone to sticking when in contact with corona-treated PET. Optimize roller materials based on production requirements: 1. Silicone rubber covered rollers: Excellent release property with low affinity to LMWOM, the preferred choice for anti-sticking. 2. Anti-stick textured tape for guide rollers: A cost-effective solution. Clean rollers with anhydrous alcohol before wrapping to avoid blistering. 3. PTFE coated rollers: Higher cost but superior durability and stable anti-sticking performance, ideal for rollers installed before and after high-temperature ovens. 4.3 Roller Parallelism & PressureExcessively small or uneven gaps between back rollers and coating rollers increase contact pressure, crushing LMWOM and causing adhesion. Use a feeler gauge to check and adjust gaps at both ends of rollers. Maintain air pressure of back pressure rollers within the specified process range. 4.4 Guide Roller Cleaning & Film PathAdhesive residue, oil stains and dust on guide rollers increase friction and cause sticking. Establish standardized operating procedures (SOP) for regular roller cleaning. Pay extra attention to small-diameter rollers such as micro-gravure rollers and back pressure rollers in micro-gravure coating systems.
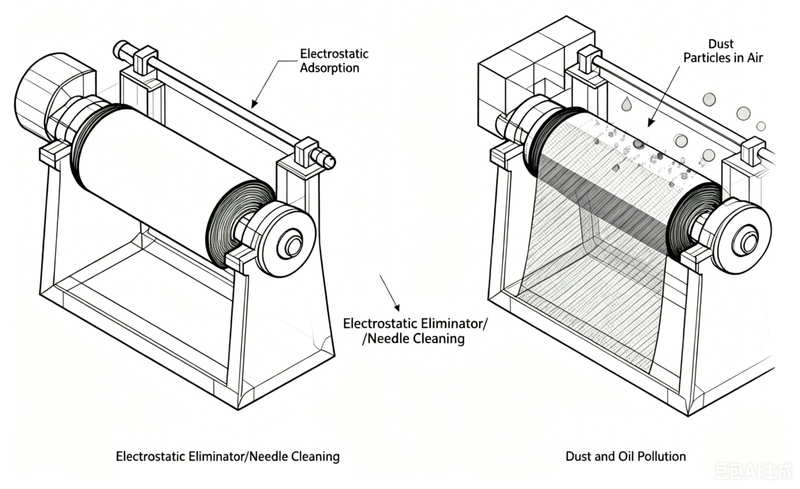
V. Production Environment & Static ElectricityEnvironmental factors are easily overlooked but play a vital role in this issue. 5.1 Temperature & Humidity·Low humidity: Static electricity generated by film friction cannot dissipate, causing the film to cling to rollers. ·High humidity: Polar groups on corona-treated film absorb moisture, softening the film surface and increasing tackiness. It is recommended to install independent temperature and humidity monitors near the coating head, as local conditions often differ from the overall workshop environment. 5.2 Static Electricity AccumulationPET is an excellent insulator. Friction during operation generates massive static charges, and dual-polarity charging is common on PET film. The electrostatic attraction is strong enough to make the film adhere tightly to rollers. Install static eliminators at key positions around coating rollers and conduct regular maintenance. Clean the needles of static eliminators with alcohol cotton when dust accumulates, as dirty needles will sharply reduce static elimination efficiency. 5.3 Environmental CleanlinessCorona-treated PET with high surface energy acts like a dust collector. Dust and oil mist in unclean workshops adhere to the film, embed into roller surfaces and gradually form permanent adhesion points. Final RemarksIn essence, PET roller sticking after corona treatment results from three interacting factors: the thickness of LMWOM generated by corona treatment, the surface condition of rubber rollers, and the pressure & temperature during film transportation. The combination of these three factors will inevitably lead to sticking failures. Master dyne level testing, fully understand the weak boundary layer mechanism, and manage rubber rollers as regularly maintained consumables. Most roller sticking problems can be resolved systematically.
With years of in-depth experience in adhesive coating production, CX Label-Zhongshan Changxin Adhesive Product Co., Ltd. has built extremely mature and stable coating processes targeting corona-treated PET film. Our professional technical team has fully summarized and optimized the full-set solutions for PET corona treatment, LMWOM control, roller maintenance, static elimination and environmental management. We effectively avoid common failures such as film winding and roller sticking, ensure continuous stable production, minimize downtime and product loss, and deliver reliable product quality and high production efficiency for all production lines. Materials Inquiry: yaozhang@changxinlabel.com Whatsapp: +852 64348733 Wechat: +86 13660700818 Keywords: Self-adhesive Label Material, Self adhesive Label Material Manufacturer, factory, tape, double-sided tape, PET Label, Overlaminate Label, Bespoke Label, Functional Label Material, Manufacturer in China, Real Factory, CX Label |